Foxy Green Foxbody Build

I know BAM will custom make a set of lifters the correct size to suit your lifter bore size for people that need a specific lifter clearance. So if someones lifter bores are currently too big on the clearance they make you a set of lifters oversize to make up for it. I'm sure they must do the same the opposite way and can go smaller.

I wonder if Johnson could also remove 0.0010 diameter (or whatever it might need) from his lifters, at a cost. Seeing as they were already able to remove some material from one of the lifters. Beats removing the engine again if he finds there's not enough clearance.
 
If damn near every lifter you buy should measure 8.740 and the shortblock guys assembled it "ready for your parts" at 8.750" bore knowing that minimum clearance is .0012" I don't know how people stay in business.

I think the easiest thing for me to do is buy the .8752 no go gauge and if it doesn't fit someone can bring a trailer
 
From the Technical Notes:

NOTE: Due to variations in lifter sizes and clearance preference, most of our engine builder customers prefer the lifter bores sized on the small size of the specification. Sometime these bores will need to be lightly honed. The lifter bore spec is .8747”-.8757”. Most lifter manufacturers recommend .0015”-.002” clearance. ALLWAYS CHECK lifter to bore clearance.

So if the bores were at Dart's max spec if would hit Johnson's spec on the bigger lifter, and you might have lifters that are a tenth more than that one.
I have to think good engine builders hit - or at least check - the bores to avoid problems like this.

Ha, treed 'cause I wandered away before hitting post! :LOL:
 
If damn near every lifter you buy should measure 8.740 and the shortblock guys assembled it "ready for your parts" at 8.750" bore knowing that minimum clearance is .0012" I don't know how people stay in business.

I think the easiest thing for me to do is buy the .8752 no go gauge and if it doesn't fit someone can bring a trailer

Fuck it, flex-hone it upside down!

Have a helper spray the flex-hone fluid through the top (bottom) while you're running the brush through.

(If that's possible, I have no idea what one of those things looks like inside...)
 
Fuck it, flex-hone it upside down!

Have a helper spray the flex-hone fluid through the top (bottom) while you're running the brush through.

(If that's possible, I have no idea what one of those things looks like inside...)

Pulling the engine is an absolute fuck you im not doing it. I'm passed that point.
 
If damn near every lifter you buy should measure 8.740 and the shortblock guys assembled it "ready for your parts" at 8.750" bore knowing that minimum clearance is .0012" I don't know how people stay in business.

I think the easiest thing for me to do is buy the .8752 no go gauge and if it doesn't fit someone can bring a trailer

because the average person buying the short block does not know better, or do they probably care about .0002 . to be honest, i would have taken the lifter and used a sharpening stone to take the edge off.

America is a wasteful society, only happy and content with the now, not the long objective. as long as it satisfies there needs RIGHT NOW, thats all that matters and thats how many scab places stay in business.
 
I think you mentioned a 1-2-3 block, which I've never used but sound like they work.
They are not ground to gage block accuracy, usually less than .001 variance but not good enough to set a gage by.

Realistically, though, if you buy a quality 0"-1" micrometer and just zero it you're probably fine.
I bet millions of guys have done that.
This. Close the mic on a piece of tablet paper, slide the paper out to clean the anvils, then make sure the thimble reads zero when you close it. I think Fox has one, but not where he is right now?

Anyway, if you measure the bore and the lifter with the same tool(micrometer) it doesn't matter how far off that tool is at zero, only what the difference is between the 2 parts. That's a good reason not to involve a bore gage here.
 
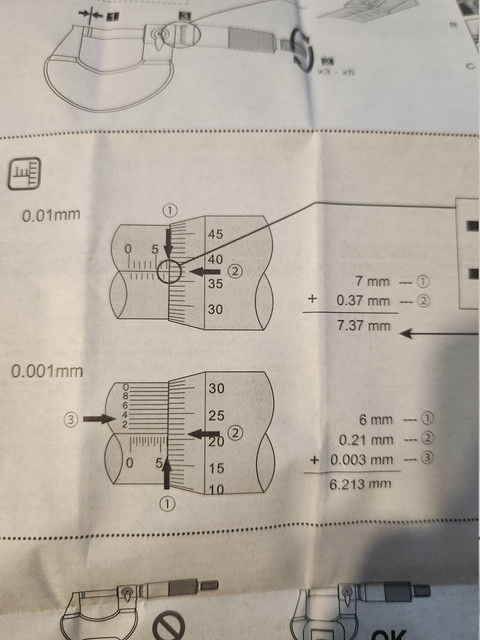
@Steve439 I don't know how to read this mm piece of shit I've been staring at it trying to understand how the big wheel only goes to 50 like I have to do math for the other 50 I'm so confused
 
So this is supposed to mean it's 0.995mm? I think I'm lost that can't be right. What the actual fuck? I thought metric system was easier

 
Instructions are even more confusing. 6.213mm?

Where the fuck did they pull the 3 out of, it doesn't line up with anything

 
I don't about the .003, other than it appears to be the only number that is in perfect alignment with a corresponding .20 line (I zoomed in and none of the other lines right perfectly line up except .003)
🤷‍♂️
 
I don't about the .003, other than it appears to be the only number that is in perfect alignment with a corresponding .20 line (I zoomed in and none of the other lines right perfectly line up except .003)
🤷‍♂️
Those lines on the barrel are vernier lines, the 3 is the first one that lines up with any other line, so you add 3 tenths to the primary measurement.

So this is supposed to mean it's 0.995mm? I think I'm lost that can't be right. What the actual fuck? I thought metric system was easier

That's .094 plus a few tenths, look further up on the barrel and see which vernier line matches up with a line on the thimble, that will tell you how many more tenths to add to the .094. Yes it's complicated and not intuitive. I'm gonna guess it's about .008.

~Edited the numbers
 
Last edited:
Back
Top